
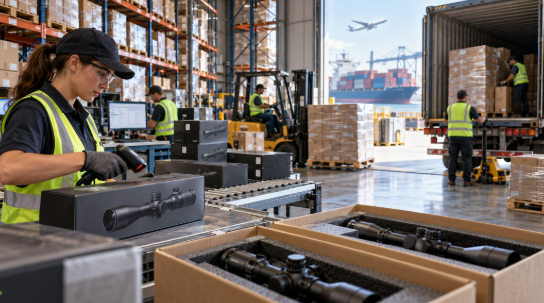
When customers explore a collection of scopes and sights, they usually focus on the finished products displayed in a store or online catalogue. They may compare designs, prices, specifications, and brand names without thinking about the complicated journey behind each item. Before optical equipment reaches a retailer, numerous businesses and professionals may be involved in sourcing materials, coordinating production, organizing shipments, and managing inventory.
Understanding this process is particularly useful for businesses working in the outdoor equipment industry. Manufacturers such as Billings scopes and sights operate within a market where optical production and business-to-business relationships play important roles. For distributors, retailers, and emerging brands, a dependable supply chain is essential for keeping products available, managing costs, and meeting customer expectations. The journey from factory to store shelf reveals why successful optical businesses depend on much more than their product catalogues.
What Is a Supply Chain in the Optical Equipment Industry?
A supply chain is the network of businesses, resources, and activities involved in producing and delivering a product.
In the optical equipment industry, this network may include material suppliers, component manufacturers, assembly facilities, shipping providers, distributors, and retailers.
Each participant contributes to moving the product toward its final destination.
A manufacturer may depend on several suppliers for different components. Once production is complete, logistics companies may transport finished goods to warehouses or distribution centers.
Retailers then make those products available to customers.
Although the process sounds straightforward, coordinating these activities requires careful planning.
A delay at one stage can affect the businesses that depend on the following stages.
This is why supply chain management remains an important part of the modern optics industry.
Where the Journey of an Optical Product Begins
The journey starts long before finished equipment is placed inside retail packaging.
Manufacturers need access to appropriate materials and components before production can begin.
Depending on the product design, these materials may include optical glass, aluminum alloys, plastic components, seals, and electronic parts.
Different suppliers may specialize in particular materials or production processes.
For example, a business producing optical equipment may obtain some components from external suppliers while manufacturing other parts internally.
The exact arrangement depends on the manufacturer’s capabilities and commercial requirements.
Reliable sourcing helps businesses maintain production schedules and meet agreed product specifications.
However, sourcing decisions involve more than finding the lowest available price.
Material suitability, supplier communication, availability, and documented requirements can all influence long-term business relationships.
Why Supplier Relationships Matter
A manufacturer may work with the same suppliers over many years.
These relationships can make communication easier, particularly when production requirements change or unexpected problems occur.
Reliable suppliers should understand the agreed specifications and communicate clearly about their ability to fulfill orders.
For manufacturers, consistency is especially important when different production batches must meet the same requirements.
Supplier relationships can also influence production planning.
If a particular material becomes unavailable, manufacturers may need additional time to identify an appropriate alternative.
Changing a component is not always a simple decision, especially when the new material requires further evaluation.
Strong supplier relationships help businesses address these challenges through communication and realistic planning.
How Production Scheduling Affects Product Availability
Manufacturing facilities often handle several product models or customer orders.
Each order may involve different materials, quantities, and delivery expectations.
Production scheduling helps organize these activities so that available resources are used effectively.
Businesses must consider component availability, equipment capacity, staff requirements, and planned inspections.
Unexpected circumstances can still interrupt production.
For example, a delayed component shipment may affect the timing of a particular production batch.
Good scheduling cannot eliminate every disruption, but it can help manufacturers identify potential problems earlier.
Retailers benefit when manufacturers provide realistic delivery information rather than making promises that cannot be supported.
Accurate schedules make inventory planning more manageable throughout the supply chain.
The Importance of Product Identification and Traceability
As products move through manufacturing and distribution, accurate identification becomes increasingly important.
Businesses need to know which products belong to particular orders and how those items should be recorded.
Depending on the company’s systems, product identification may involve model numbers, production batches, barcodes, or serial numbers.
These records can support inventory management and help businesses investigate product concerns.
A well-organized traceability system may make it easier to identify which shipment or production batch is associated with a reported issue.
Not every product uses the same identification process.
However, clear records can reduce confusion when businesses handle several similar models.
Traceability is particularly valuable when products pass through multiple warehouses, distributors, or retail locations.
Why Communication Connects the Entire Supply Chain
Even a well-planned supply chain can encounter difficulties when communication breaks down.
Manufacturers, distributors, and retailers need accurate information about orders, specifications, shipment schedules, and product availability.
Companies such as Billings scopes and sights work in an industry where optical manufacturers may support distributors, equipment brands, and commercial customers. The company’s published information describes its optical manufacturing operations and OEM and ODM services, highlighting the variety of business relationships involved in this market.
For companies working with manufacturing partners, communication should continue throughout the ordering and delivery process.
Important information may include:
- Order confirmation: Clearly identifying the products and quantities requested.
- Production updates: Sharing meaningful changes to agreed schedules.
- Product documentation: Providing accurate specifications and identification details.
- Shipping arrangements: Confirming transportation responsibilities and delivery expectations.
- Inventory information: Communicating product availability and possible shortages.
- After-sales procedures: Explaining how reported product concerns will be handled.
These practices can help businesses avoid misunderstandings and maintain more dependable relationships.
How International Shipping Influences the Industry
Optical products are often manufactured, distributed, and sold across different countries.
International transportation introduces additional considerations, including freight arrangements, customs documentation, and delivery schedules.
Shipping methods vary depending on shipment size, destination, cost, and urgency.
Air freight may offer shorter transit times, while ocean freight can be more economical for suitable larger shipments.
However, actual costs and delivery times depend on several factors.
Businesses also need to consider applicable import and export regulations.
Certain optical products or accessories may be subject to additional restrictions depending on their specifications and destination.
Importers should therefore verify classification, documentation, and legal requirements with qualified professionals before arranging shipments.
Careful preparation helps reduce avoidable transportation problems.
Why Packaging Matters During Transportation
A finished optical product may travel considerable distances before reaching a customer.
During transportation, packages can experience vibration, movement, stacking pressure, and changing environmental conditions.
Appropriate packaging helps protect products from avoidable damage.
Manufacturers and distributors may use protective inserts, fitted cartons, and suitable outer packaging depending on the products being shipped.
Packaging also supports accurate order handling.
Clearly marked product identifiers can help warehouse teams distinguish between different models.
However, packaging should be appropriate rather than excessive.
Businesses need to balance protection, transportation efficiency, material use, and practical handling.
A well-organized packaging approach can support smoother movement through the supply chain.
The Role of Warehouses and Distribution Centers
Warehouses are more than temporary storage spaces.
They help businesses receive shipments, organize stock, prepare orders, and manage product availability.
A distributor may carry several optical product categories from different manufacturers.
Accurate inventory systems make it easier to identify available quantities and avoid confusion between similar models.
Warehouse processes can also influence how efficiently retailers receive their orders.
For example, incorrect labeling or stock records may cause delays even when the required products are physically available.
Regular inventory checks help businesses identify differences between recorded and actual stock levels.
Organized storage and handling procedures are therefore important parts of reliable distribution.
How Retailers Manage Changing Customer Demand
Customer demand is not always consistent throughout the year.
Outdoor equipment retailers may experience changes in purchasing patterns influenced by local seasons, market conditions, and consumer preferences.
Businesses must decide how much stock to carry without creating unnecessary storage costs.
Ordering too little inventory can leave customers waiting for products.
Ordering too much may create financial pressure and increase the risk of unsold stock.
Retailers can use past sales information, supplier lead times, and current market observations to make more informed decisions.
However, forecasts are never perfect.
Maintaining communication with distributors and manufacturers can help retailers respond when actual demand differs from expectations.
Why Delivery Reliability Builds Business Confidence
For commercial buyers, dependable delivery can be just as important as an attractive product catalogue.
Retailers often plan promotions, product launches, and purchasing commitments around expected stock availability.
Unexpected delays may affect these plans and create additional work.
Reliable suppliers do not necessarily promise the fastest possible delivery.
Instead, they provide realistic information and communicate meaningful changes.
Businesses should understand the difference between an estimated production date, shipment date, and final delivery date.
These stages are not interchangeable.
Clearly explaining them helps commercial customers plan their operations with fewer misunderstandings.
Over time, dependable communication can strengthen confidence between supply chain partners.
Managing Returns and Product Concerns
The supply chain does not always end when a product is delivered.
Businesses may need to manage damaged shipments, incorrect orders, warranty requests, or other customer concerns.
These situations require clear procedures.
Retailers should understand whom to contact, which documentation is required, and how a reported issue will be evaluated.
Manufacturers and distributors may establish different responsibilities depending on their commercial agreements.
Accurate records can help identify the products involved and determine the appropriate next steps.
Customer feedback may also reveal recurring problems with packaging, labeling, or order handling.
Reviewing these concerns can help businesses improve future processes.
A dependable supply chain includes the ability to address problems professionally, not simply deliver goods.
How Digital Systems Are Changing Supply Chain Management
Digital tools have become valuable for businesses managing products across multiple locations.
Inventory software, electronic order records, and shipment tracking systems can help companies organize information more efficiently.
These systems may reduce the need for repeated manual updates and make important details easier to access.
However, technology alone does not guarantee accurate information.
Businesses still need reliable procedures for recording stock movements, updating orders, and communicating changes.
A simple system used consistently may provide greater practical value than an expensive platform that staff members struggle to maintain.
Digital improvements are most useful when they support clear responsibilities and established business processes.
Conclusion
The journey of optical equipment from manufacturing facilities to retail shelves involves a network of suppliers, logistics providers, distributors, and retailers. Every stage contributes to product availability and the overall customer experience. Businesses interested in exploring optical manufacturing and related product categories can learn more through billingsoptics.com, which provides information about scopes, sights, and manufacturing services. Understanding the wider supply chain helps businesses recognize the importance of dependable commercial relationships.
Successful supply chain management is built on realistic planning, accurate information, clear communication, and organized delivery procedures. While customers usually see only the finished optical product, the work taking place behind the scenes helps determine whether that product reaches the market efficiently. For manufacturers and retailers alike, investing attention in these processes can support stronger partnerships, more reliable operations, and greater long-term business confidence.